• +91 9664106499
  • gandhimetalindia@gmail.com

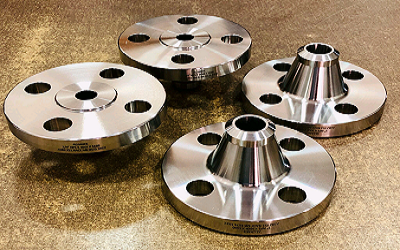
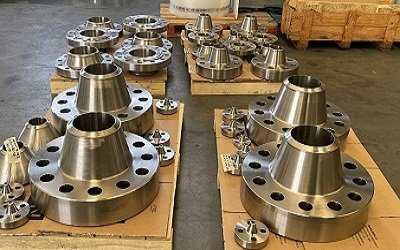
Stainless Steel 321H Flanges

Stainless Steel Flanges Specifications

Material Grades

  • Stainless Steel 304 / 304L / 304H
  • Stainless Steel 310 / 310S
  • Stainless Steel 316 / 316L / 316H
  • Stainless Steel 317 / 317L
  • Stainless Steel 321 / 321H
  • Stainless Steel 347 / 347H
  • Stainless Steel 446
  • Stainless Steel 904L

Forging Method

  • Closed Die Forging
  • Hot Forging
  • Impression Die Forging
  • Cold Forging
  • Open Die Forging
  • Drop Forging
  • Upset Forging

Flange Testing

  • Radiography Testing
  • Ultrasonic Testing
  • Liquid Penetrant Testing
  • Non-Destructive Testing (NDT)
  • Positive Material Identification (PMI)
  • Dimensional Inspection

Value Added Services

  • Heat Treatment
  • Solution Annealing
  • Pickling & Passivation
  • Shot Blasting
  • Machining
  • Custom Finishing

Manufacturing Standards

  • ASME B16.5
  • ASME B16.47 Series A & B
  • MSS SP-44
  • API 605
  • AWWA Standards
  • ASA Standards
  • Custom Drawings

Flanges Sizes

  • Size: 1/2" – 60"
  • Pressure Class: 150 – 2500 LBS
  • Pressure Rating: PN6 – PN64
  • Faces: FF, RF & RTJ

Chemical Composition

Carbon (C)
0.04 – 0.10%
Manganese (Mn)
2.00% Max
Silicon (Si)
1.00% Max
Phosphorus (P)
0.045% Max
Sulfur (S)
0.030% Max
Chromium (Cr)
17.00 – 19.00%
Nitrogen (N)
0.10% Max
Nickel (Ni)
9.00 – 12.00%
Titanium (Ti)
4(C+N) – 0.70%

Physical Properties

Grade Stainless Steel 321H
UNS S32109
Werkstoff No. 1.4878
JIS SUS 321H
EN X12CrNiTi18-9
Density 8.0 g/cm3
Melting Point 1457 °C (2650 °F)
Standard ASTM A182 / A240 & ASME SA182 / SA240
Size Range ½″ to 48″
Pressure Class 150# to 2500# / PN6 to PN64
Tensile Strength
515 MPa
75,000 Psi
Yield Strength
205 MPa
30,000 Psi
Elongation
35 %
Minimum Elongation
Melting Point
1457 °C
2650 °F


MANUFACTURING

Forging Process

Each flange follows a rigorous 8-step forging and quality-control process to ensure conformance with ASTM A182 and ASME standards.

1

Material Selection

Prime 304 stainless steel billet sourced and certified.

2

Billet Preparation

Heat to 1100°C – 1250°C for optimal forgeability.

3

Forging

Shape billet into flange geometry under controlled pressure.

4

Heat Treatment

Solution anneal at 1040°C – 1120°C, then quench.

5

Machining & Finishing

CNC machining, drilling, and surface finishing.

6

Testing & Inspection

Tensile, hardness, PMI, visual and impact tests performed.