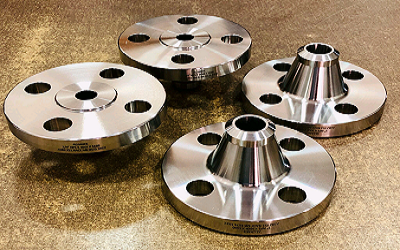
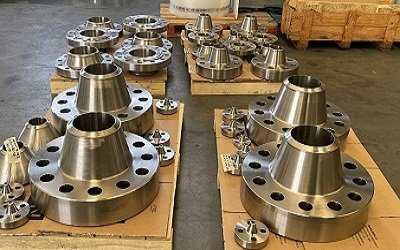
| NPS | Bolt Circle (mm) | Flange O.D. (mm) | Thickness (mm) | Bolt Hole Ø (mm) | No. Of Bolts |
|---|---|---|---|---|---|
| ½″ | 60.45 | 88.90 | 9.65 | 15.75 | 4 |
| ¾″ | 69.85 | 98.55 | 11.18 | 15.75 | 4 |
| 1″ | 79.25 | 107.95 | 12.70 | 15.75 | 4 |
| 1¼″ | 88.90 | 117.35 | 14.22 | 15.75 | 4 |
| 1½″ | 98.55 | 127.00 | 15.75 | 15.75 | 4 |
| 2″ | 120.65 | 152.40 | 17.53 | 19.05 | 4 |
| 2½″ | 139.70 | 177.80 | 20.57 | 19.05 | 4 |
| 3″ | 152.40 | 190.50 | 22.35 | 19.05 | 4 |
| 3½″ | 177.80 | 215.90 | 22.35 | 19.05 | 8 |
| 4″ | 190.50 | 228.60 | 22.35 | 19.05 | 8 |
| 5″ | 215.90 | 254.00 | 22.35 | 22.35 | 8 |
| 6″ | 241.30 | 279.40 | 23.88 | 22.35 | 8 |
| 8″ | 298.45 | 342.90 | 26.92 | 22.35 | 8 |
| 10″ | 361.95 | 406.40 | 28.45 | 25.40 | 12 |
| 12″ | 431.80 | 482.60 | 30.23 | 25.40 | 12 |
Each flange follows a rigorous 8-step forging and quality-control process to ensure conformance with ASTM A182 and ASME standards.
Prime 304 stainless steel billet sourced and certified.
Heat to 1100°C – 1250°C for optimal forgeability.
Shape billet into flange geometry under controlled pressure.
Solution anneal at 1040°C – 1120°C, then quench.
CNC machining, drilling, and surface finishing.
Tensile, hardness, PMI, visual and impact tests performed.