• +91 9664106499
  • gandhimetalindia@gmail.com

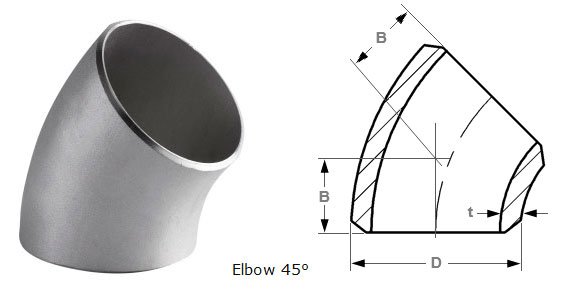
45° Long Radius Elbow

SPECIFICATIONS

Product Type

  • Butt Weld 45° Long Radius Elbow
  • 45 Degree LR Elbow
  • Long Radius Elbow
  • Butt Weld Pipe Elbow
  • Seamless Butt Weld Elbow
  • Welded Butt Weld Elbow

Material Grades

  • ASTM A403 WP304 / WP304L
  • ASTM A403 WP316 / WP316L
  • ASTM A182 F304 / F316
  • ASTM A815 S31803 / S32205
  • ASTM A234 WPB
  • ASTM A420 WPL3 / WPL6
  • ASTM A234 WP5 / WP9 / WP11 / WP22 / WP91
  • Nickel & Copper Nickel Alloys

Manufacturing Standards

  • ASME / ANSI B16.9
  • ASME B16.25
  • ASME B16.28
  • MSS SP-43
  • JIS B2312
  • JIS B2313

Size Range

  • Size: 1/2" to 36"
  • Seamless: Up to 24"
  • Welded: 8" to 36"
  • Nominal Pipe Size (NPS)
  • Custom Sizes Available

Thickness & Schedule

  • Schedule 5S
  • Schedule 10S
  • Schedule 20
  • Schedule 40 / STD
  • Schedule 60
  • Schedule 80 / XS
  • Schedule 100 / 120 / 140
  • Schedule 160 / XXS

Elbow Configuration

  • 45° Long Radius
  • 1.5D Radius Configuration
  • Equal End Diameters
  • Butt Weld Ends
  • Center-to-End Dimensions
  • Controlled Flow Direction Change

Dimensional Tolerances

  • Outside Diameter at Bevel
  • Inside Diameter at End
  • Center-to-End Tolerance
  • Wall Thickness Tolerance
  • Angular Tolerance
  • End Alignment Tolerance

End Preparation

  • Butt Weld Ends
  • Beveled Ends
  • ASME B16.25 End Preparation
  • Weldable Pipe Ends
  • Precision End Preparation

Manufacturing Process

  • Hot Forming
  • Cold Forming
  • Seamless Construction
  • Welded Construction
  • Heat Treatment
  • Precision Forming

Inspection & Testing

  • Visual Inspection
  • Dimensional Inspection
  • Material Verification
  • Surface Inspection
  • Quality Inspection

45 Degree Long Radius Elbow Dimensions Chart

NPS Outside Diameter (D) (mm) 45° Long Radius Center-to-End (B) (mm) 45° 3D Center-to-End (B) (mm)
½″21.316–
¾″26.71924
1″33.42231
1¼″42.22539
1½″48.32947
2″60.33563
2½″73.04479
3″88.95195
3½″101.657111
4″114.364127
5″141.379157
6″168.395189
8″219.1127252
10″273.0159316
12″323.8190378
14″355.6222441
16″406.4254505
18″457.0286568
20″508.0318632
22″559.0343694
24″610.0381757
26″660.0406821
28″711.0438883
30″762.0470964
32″813.05021010
34″864.05331073
36″914.05651135
38″965.06001200
40″1016.06321264
42″1067.06601326
44″1118.06951389
46″1168.07271453
48″1219.07591516


MANUFACTURING

Forging Process

Each flange follows a rigorous 8-step forging and quality-control process to ensure conformance with ASTM A182 and ASME standards.

1

Material Selection

Prime 304 stainless steel billet sourced and certified.

2

Billet Preparation

Heat to 1100°C – 1250°C for optimal forgeability.

3

Forging

Shape billet into flange geometry under controlled pressure.

4

Heat Treatment

Solution anneal at 1040°C – 1120°C, then quench.

5

Machining & Finishing

CNC machining, drilling, and surface finishing.

6

Testing & Inspection

Tensile, hardness, PMI, visual and impact tests performed.