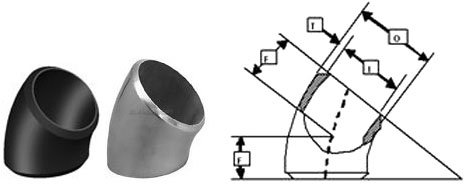
Nom. Pipe Size | Pipe Sched. or No. | Center- to-end Dimen. | Outside Dia. | Inside Dia. | Wall Thick. | Approx. Weight (lb.) |
|---|---|---|---|---|---|---|
| F | OD | ID | T | |||
| STANDARD WEIGHT | ||||||
| 1/2 | 40 | 5/8 | 0.840 | 0.622 | 0.109 | 0.1 |
| 3/4 | 40 | 7/16 | 1.050 | 0.824 | 0.113 | 0.1 |
| 1 | 40 | 7/8 | 1.315 | 1.049 | 0.133 | 0.2 |
| 1 1/4 | 40 | 1 | 1.660 | 1.380 | 0.140 | 0.4 |
| 1 1/2 | 40 | 1 1/8 | 1.900 | 1.610 | 0.145 | 0.5 |
| 2 | 40 | 1 3/8 | 2.375 | 2.067 | 0.154 | 0.9 |
| 2 1/2 | 40 | 1 3/4 | 2.875 | 2.469 | 0.203 | 1.5 |
| 3 | 40 | 2 | 3.500 | 3.068 | 0.216 | 2.5 |
| 3 1/2 | 40 | 2 1/4 | 4.000 | 3.548 | 0.226 | 3.5 |
| 4 | 40 | 2 1/2 | 4.500 | 4.026 | 0.237 | 4.8 |
| 5 | 40 | 3 1/8 | 5.563 | 5.047 | 0.258 | 7.8 |
| 6 | 40 | 3 3/4 | 6.625 | 6.065 | 0.280 | 12 |
| 8 | 40 | 5 | 8.625 | 7.981 | 0.322 | 23 |
| 10 | 40 | 6 1/4 | 10.750 | 10.020 | 0.365 | 42 |
| 12 | – | 7 1/2 | 12.750 | 12.000 | 0.375 | 61 |
| 14 | 30 | 8 3/4 | 14.000 | 13.250 | 0.375 | 79 |
| 16 | 30 | 10 | 16.000 | 15.250 | 0.375 | 103 |
| 18 | – | 11 1/4 | 18.000 | 17.250 | 0.375 | 132 |
| 20 | 20 | 12 1/2 | 20.000 | 19.250 | 0.375 | 160 |
| 22 | 20 | 13 1/2 | 22.000 | 21.250 | 0.375 | 195 |
| 24 | 20 | 15 | 24.000 | 23.250 | 0.375 | 238 |
Each flange follows a rigorous 8-step forging and quality-control process to ensure conformance with ASTM A182 and ASME standards.
Prime 304 stainless steel billet sourced and certified.
Heat to 1100°C – 1250°C for optimal forgeability.
Shape billet into flange geometry under controlled pressure.
Solution anneal at 1040°C – 1120°C, then quench.
CNC machining, drilling, and surface finishing.
Tensile, hardness, PMI, visual and impact tests performed.