ASTM A403 WP304 / WP304L
ASTM A403 WP316 / WP316L
ASTM A815 Duplex & Super Duplex
ASTM A234 Carbon Steel
ASTM A420 Low Temperature Steel
Nickel Alloys
Inconel, Incoloy, Monel & Hastelloy
Lap Joint Stub End
Butt Weld Stub End
Long Pattern Stub End
Short Pattern Stub End
Seamless Stub End
Welded Stub End
ASME B16.9
ASME B16.25
MSS SP-43
ASTM A403
ASTM A815
ASTM A234
JIS B2312 / JIS B2313
NPS 1/2" to 24"
DN 15 to DN 600
Long Pattern
Short Pattern
Custom Sizes Available
3 mm to 40 mm
Schedule 5S
Schedule 10S
Schedule 40S / STD
Schedule 80S / XS
Schedule 160
XXS & Custom Thickness
Butt Weld Connection
Lap Joint Flange Connection
Beveled Welding End
ASME B16.25 End Preparation
Seamless
Welded
Hot Formed
Cold Formed
Machined & Finished
Solution Annealed
Pickled & Passivated
Shot Blasted
Machined Finish
Polished Finish
As Manufactured
Visual Inspection
Dimensional Inspection
PMI Testing
Hardness Testing
Radiographic Testing
Ultrasonic Testing
Third Party Inspection
EN 10204 3.1 Certificate
Material Test Certificate
PMI Certificate
Certificate of Conformance
Third Party Inspection Report
Oil & Gas
Petrochemical
Chemical Processing
Power Generation
Water Treatment
Process Piping
Marine Applications
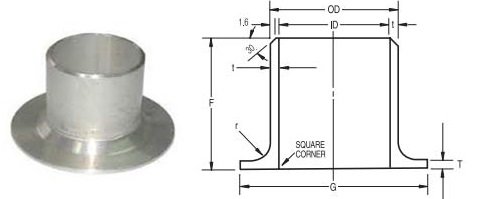
Dimensions are based on ASME B16.9. All dimensions are in mm.
| NPS | OD at Bevel | Long Pattern F | Short Pattern F | Lap Diameter G | Fillet Radius R | OD Barrel Max | OD Barrel Min |
|---|---|---|---|---|---|---|---|
| 1/2" | 21 | 76 | 51 | 35 | 3 | 23 | 21 |
| 3/4" | 27 | 76 | 51 | 43 | 3 | 28 | 26 |
| 1" | 33 | 102 | 51 | 51 | 3 | 35 | 33 |
| 1 1/4" | 42 | 102 | 51 | 64 | 5 | 44 | 41 |
| 1 1/2" | 48 | 102 | 51 | 73 | 6 | 50 | 47 |
| 2" | 60 | 152 | 64 | 92 | 8 | 62 | 60 |
| 2 1/2" | 73 | 152 | 64 | 105 | 8 | 75 | 72 |
| 3" | 89 | 152 | 64 | 127 | 10 | 91 | 88 |
| 3 1/2" | 102 | 152 | 76 | 140 | 10 | 104 | 101 |
| 4" | 114 | 152 | 76 | 157 | 11 | 117 | 114 |
| 5" | 141 | 203 | 76 | 186 | 11 | 144 | 141 |
| 6" | 168 | 203 | 89 | 216 | 13 | 171 | 168 |
| 8" | 219 | 203 | 102 | 270 | 13 | 222 | 218 |
| 10" | 273 | 254 | 127 | 324 | 13 | 277 | 272 |
| 12" | 324 | 254 | 152 | 381 | 13 | 328 | 323 |
| 14" | 356 | 305 | 152 | 413 | 13 | 360 | 355 |
| 16" | 406 | 305 | 152 | 470 | 13 | 411 | 406 |
| 18" | 457 | 305 | 152 | 533 | 13 | 462 | 456 |
| 20" | 508 | 305 | 152 | 584 | 13 | 514 | 507 |
| 22" | 559 | 305 | 152 | 641 | 13 | 565 | 558 |
| 24" | 610 | 305 | 152 | 692 | 13 | 616 | 609 |
| NPS | Schedule 5S (mm) | Schedule 10S (mm) | Schedule 40S (mm) | Schedule 80S (mm) |
|---|---|---|---|---|
| 1/2" | 1.65 | 2.11 | 2.77 | 3.73 |
| 3/4" | 1.65 | 2.11 | 2.87 | 3.91 |
| 1" | 1.65 | 2.77 | 3.38 | 4.55 |
| 1 1/4" | 1.65 | 2.77 | 3.56 | 4.85 |
| 1 1/2" | 1.65 | 2.77 | 3.68 | 5.08 |
| 2" | 1.65 | 2.77 | 3.91 | 5.54 |
| 2 1/2" | 2.11 | 3.05 | 5.16 | 7.01 |
| 3" | 2.11 | 3.05 | 5.49 | 7.62 |
| 3 1/2" | 2.11 | 3.05 | 5.74 | 8.08 |
| 4" | 2.11 | 3.05 | 6.02 | 8.56 |
| 5" | 2.77 | 3.40 | 6.55 | 9.53 |
| 6" | 2.77 | 3.40 | 7.11 | 10.97 |
| 8" | 2.77 | 3.76 | 8.18 | 12.70 |
| 10" | 3.40 | 4.19 | 9.27 | 12.70 |
| 12" | 3.96 | 4.57 | 9.53 | 12.70 |
| 14" | 3.96 | 4.78 | — | — |
| 16" | 4.19 | 4.78 | — | — |
| 18" | 4.19 | 4.78 | — | — |
| 20" | 4.78 | 5.54 | — | — |
| 22" | 4.78 | 5.54 | — | — |
| 24" | 5.54 | 6.35 | — | — |
Approximate weight for Schedule 40S / STD configuration.
| NPS | Outside Diameter (mm) | Approx. Weight (kg/piece) |
|---|---|---|
| 1/2" | 21.3 | 0.14 |
| 3/4" | 26.7 | 0.18 |
| 1" | 33.4 | 0.30 |
| 1 1/4" | 42.2 | 0.41 |
| 1 1/2" | 48.3 | 0.55 |
| 2" | 60.3 | 1.00 |
| 2 1/2" | 73.0 | 1.56 |
| 3" | 88.9 | 2.15 |
| 3 1/2" | 101.6 | — |
| 4" | 114.3 | 3.05 |
| 5" | 141.3 | 5.30 |
| 6" | 168.3 | 6.90 |
| 8" | 219.1 | 10.45 |
| 10" | 273.0 | 18.15 |
| 12" | 323.9 | 22.25 |
| 14" | 355.6 | 29.05 |
| 16" | 406.4 | 32.69 |
| 18" | 457.0 | 38.60 |
| 20" | 508.0 | 42.68 |
| 22" | 559.0 | — |
| 24" | 610.0 | 51.30 |
Reference material: ASTM A403 WP304L Stainless Steel
| Property | Value | Unit |
|---|---|---|
| Tensile Strength | 485 | MPa min. |
| Yield Strength | 170 | MPa min. |
| Elongation | 35 | % min. |
| Hardness | 92 | HRB max. |
| Brinell Hardness | 201 | HB max. |
Each flange follows a rigorous 8-step forging and quality-control process to ensure conformance with ASTM A182 and ASME standards.
Prime 304 stainless steel billet sourced and certified.
Heat to 1100°C – 1250°C for optimal forgeability.
Shape billet into flange geometry under controlled pressure.
Solution anneal at 1040°C – 1120°C, then quench.
CNC machining, drilling, and surface finishing.
Tensile, hardness, PMI, visual and impact tests performed.