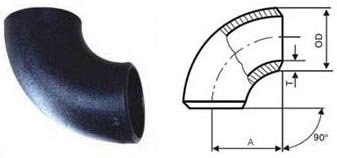
| Nominal Diameter | Outside Diameter at Bevel | Center to End | Center to Center | Back to Face | ||||||
|---|---|---|---|---|---|---|---|---|---|---|
| 45°Elbow | 90°Elbow | 180°Elbow | ||||||||
| B | A | O | K | |||||||
| DN | NPS | Series A | Series B | Long Radius | Long Radius | Short Radius | Long Radius | Short Radius | Long Radius | Short Radius |
| 15 | 1/2 | 21.3 | 18 | 16 | 38 | – | 76 | – | 48 | – |
| 20 | 3/4 | 26.9 | 25 | 19 | 38 | – | 76 | – | 51 | – |
| 25 | 1 | 33.7 | 32 | 22 | 38 | 25 | 76 | 51 | 56 | 41 |
| 32 | 1.1/4 | 42.4 | 38 | 25 | 48 | 32 | 95 | 64 | 70 | 52 |
| 40 | 1.1/2 | 48.3 | 45 | 29 | 57 | 38 | 114 | 76 | 83 | 62 |
| 50 | 2 | 60.3 | 57 | 35 | 76 | 51 | 152 | 102 | 106 | 81 |
| 65 | 2.1/2 | 76.1(73) | 76 | 44 | 95 | 64 | 190 | 127 | 132 | 100 |
| 80 | 3 | 88.9 | 89 | 51 | 114 | 76 | 229 | 152 | 159 | 121 |
| 90 | 3.1/2 | 101.6 | – | 57 | 133 | 89 | 267 | 178 | 184 | 140 |
| 100 | 4 | 114.3 | 108 | 64 | 152 | 102 | 305 | 203 | 210 | 159 |
| 125 | 5 | 139.7 | 133 | 79 | 190 | 127 | 381 | 254 | 262 | 197 |
| 150 | 6 | 168.3 | 159 | 95 | 229 | 152 | 457 | 305 | 313 | 237 |
| 200 | 8 | 219.1 | 219 | 127 | 305 | 203 | 610 | 406 | 414 | 313 |
| 250 | 10 | 273.0 | 273 | 159 | 381 | 254 | 762 | 508 | 518 | 391 |
| 300 | 12 | 323.9 | 325 | 190 | 457 | 305 | 914 | 610 | 619 | 467 |
| 350 | 14 | 355.6 | 377 | 222 | 533 | 356 | 1067 | 711 | 711 | 533 |
| 400 | 16 | 406.4 | 426 | 254 | 610 | 406 | 1219 | 813 | 813 | 610 |
| 450 | 18 | 457.2 | 478 | 286 | 686 | 457 | 1372 | 914 | 914 | 686 |
| 500 | 20 | 508.0 | 529 | 318 | 762 | 508 | 1524 | 1016 | 1016 | 762 |
| 550 | 22 | 559 | – | 343 | 838 | 559 | 1676 | 1118 | 1118 | 838 |
| 600 | 24 | 610 | 630 | 381 | 914 | 610 | 1829 | 1219 | 1219 | 914 |
| 650 | 26 | 660 | – | 406 | 991 | 660 | 1982 | 1320 | – | – |
| 700 | 28 | 711 | 720 | 438 | 1067 | 711 | 2134 | 1422 | – | – |
| 750 | 30 | 762 | – | 470 | 1143 | 762 | 2286 | 1524 | – | – |
| 800 | 32 | 813 | 820 | 502 | 1219 | 813 | 2438 | 1626 | – | – |
| 850 | 34 | 864 | – | 533 | 1295 | 864 | 2590 | 1728 | – | – |
| 900 | 36 | 914 | 920 | 565 | 1372 | 914 | 2744 | 1828 | – | – |
| 950 | 38 | 965 | – | 600 | 1448 | 965 | 2896 | 1930 | – | – |
| 1000 | 40 | 1016 | 1020 | 632 | 1524 | 1016 | 3048 | 2032 | – | – |
| 1050 | 42 | 1067 | – | 660 | 1600 | 1067 | 3200 | 2134 | – | – |
| 1100 | 44 | 1118 | 1120 | 695 | 1676 | 1118 | 3352 | 2236 | – | – |
| 1150 | 46 | 1168 | – | 727 | 1753 | 1168 | 3506 | 2336 | – | – |
| 1200 | 48 | 1220 | 1220 | 759 | 1829 | 1219 | 3658 | 2440 | – | – |
Each flange follows a rigorous 8-step forging and quality-control process to ensure conformance with ASTM A182 and ASME standards.
Prime 304 stainless steel billet sourced and certified.
Heat to 1100°C – 1250°C for optimal forgeability.
Shape billet into flange geometry under controlled pressure.
Solution anneal at 1040°C – 1120°C, then quench.
CNC machining, drilling, and surface finishing.
Tensile, hardness, PMI, visual and impact tests performed.